1 · Order reference
PO details, panel schedule, approved physical sample, colour reference, artwork and fabrication drawing are brought together before production.
Decorative resin is judged visually as well as dimensionally. Production is checked against an approved sample, drawing, panel schedule and order-specific specification rather than a generic catalogue description.
The checks below describe the production controls represented by our current records and shop photographs. Final acceptance criteria must be agreed in writing for the exact project.
PO details, panel schedule, approved physical sample, colour reference, artwork and fabrication drawing are brought together before production.
Resin and decorative components are checked against the agreed material reference. Colour, finish and sheet build are frozen for the batch.
Panel size, thickness, squareness, edge finish and machined features are compared with the approved fabrication drawing.
The visible face is reviewed for scratches, contamination, abnormal marks, lamination defects and unacceptable edge quality under agreed viewing conditions.
Where supplied, holes, cut-outs, curves and assembled sequences are checked against the schedule. Backlit assemblies are powered and reviewed for visible light gaps or hotspots.
Panel count, identification, face protection, edge protection and packing method are checked before the export package is closed.
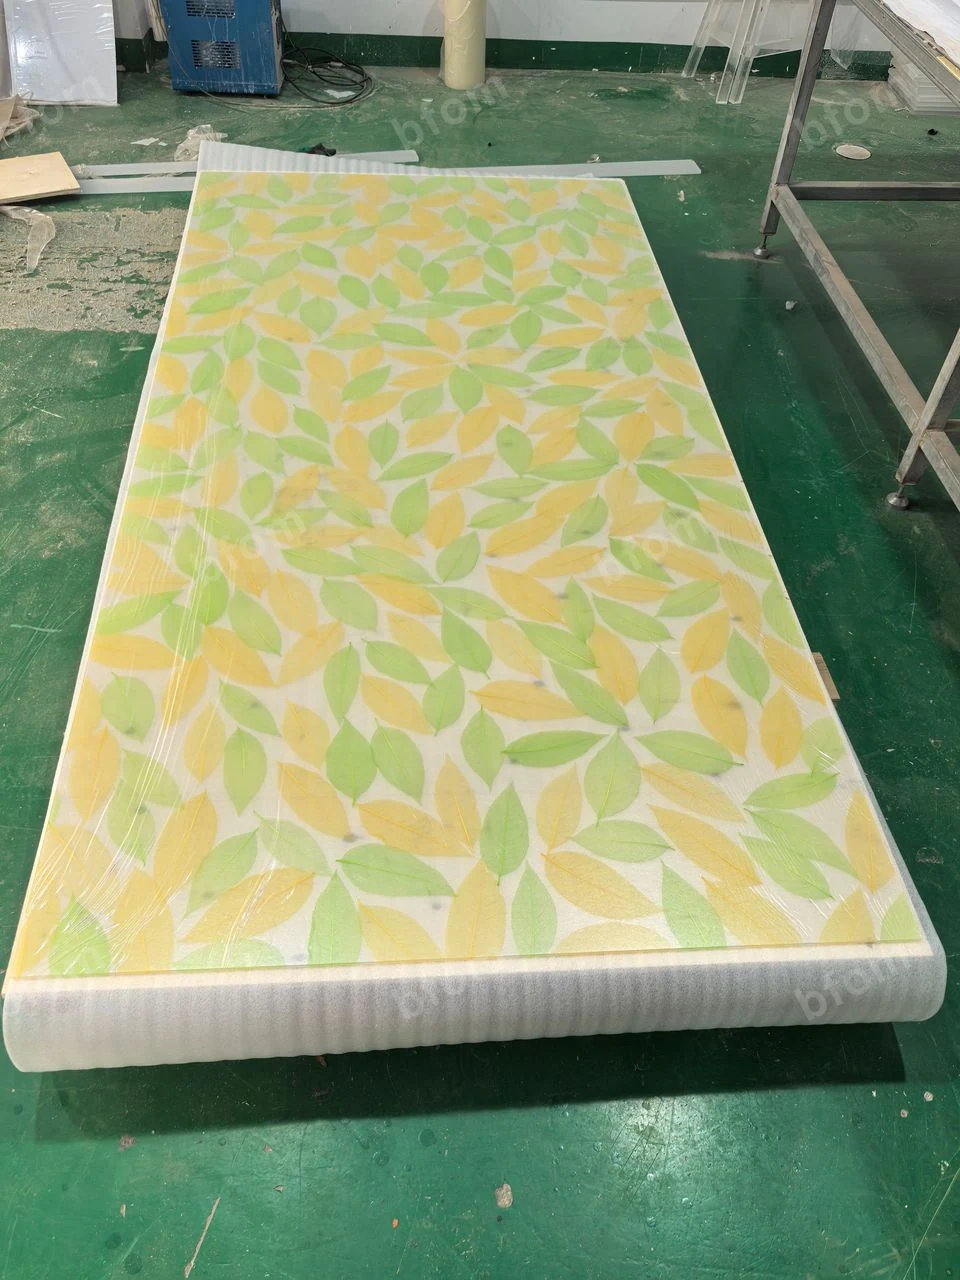
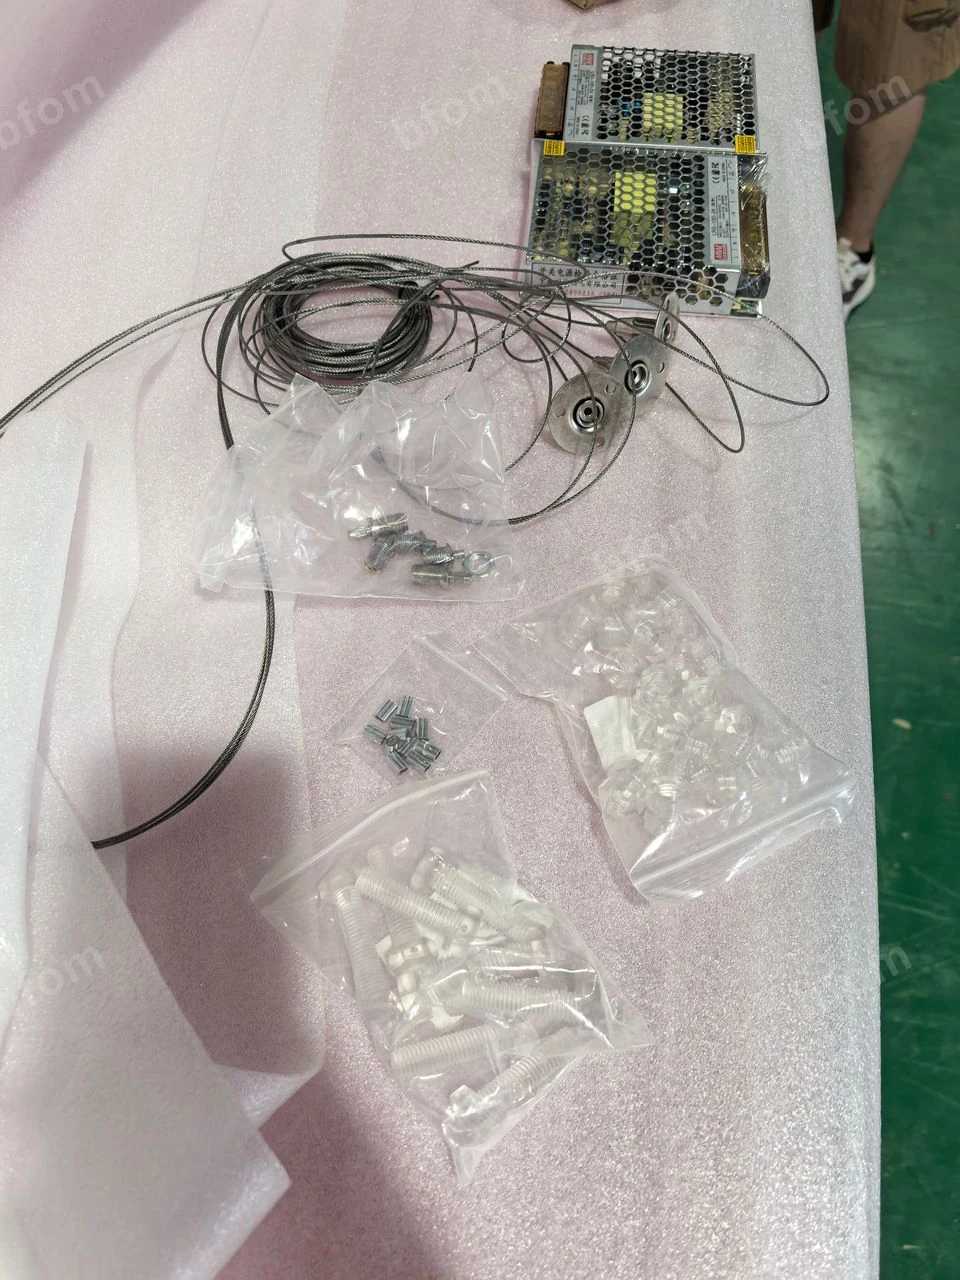
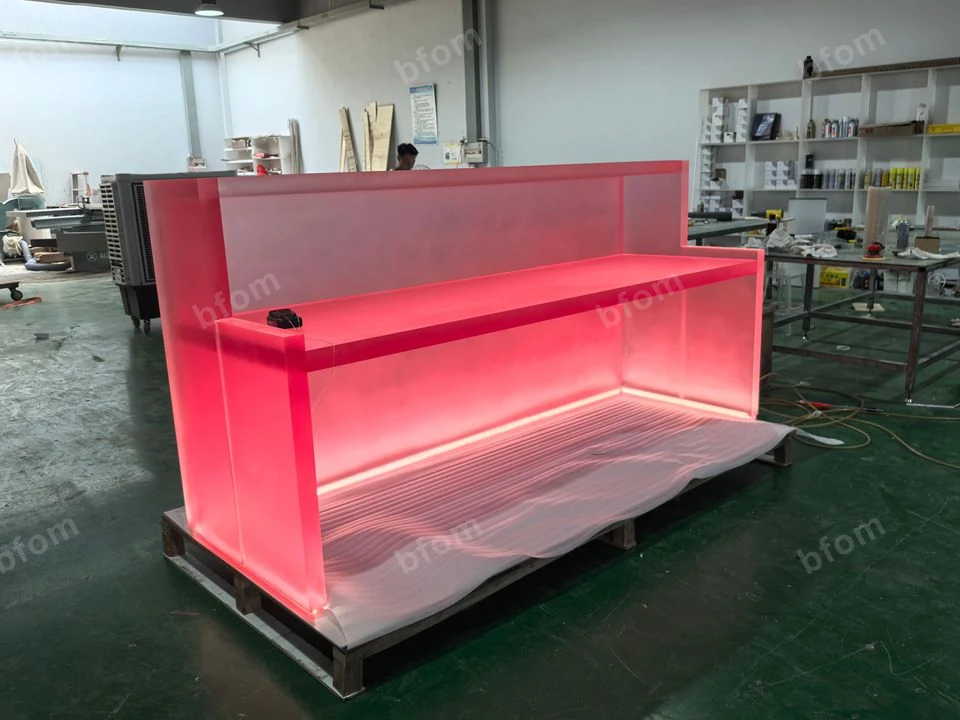
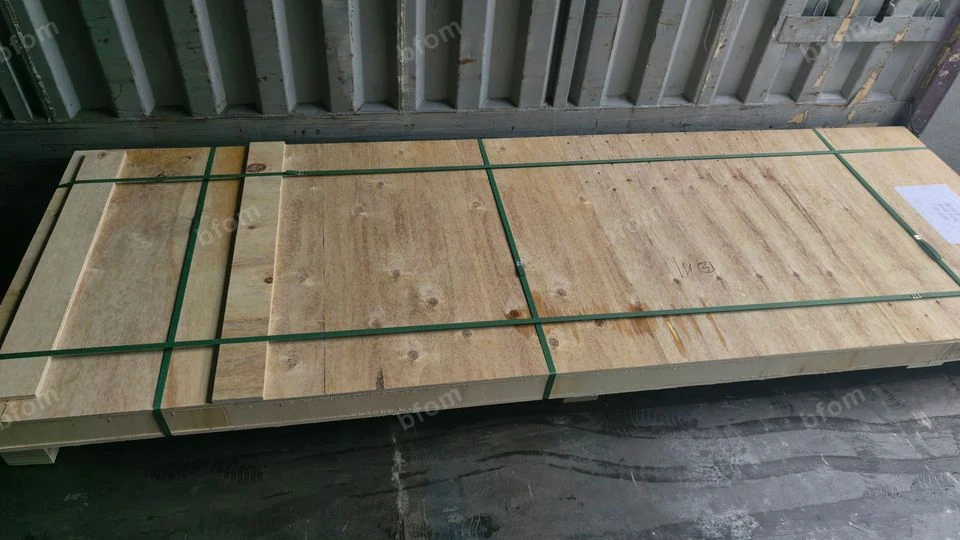
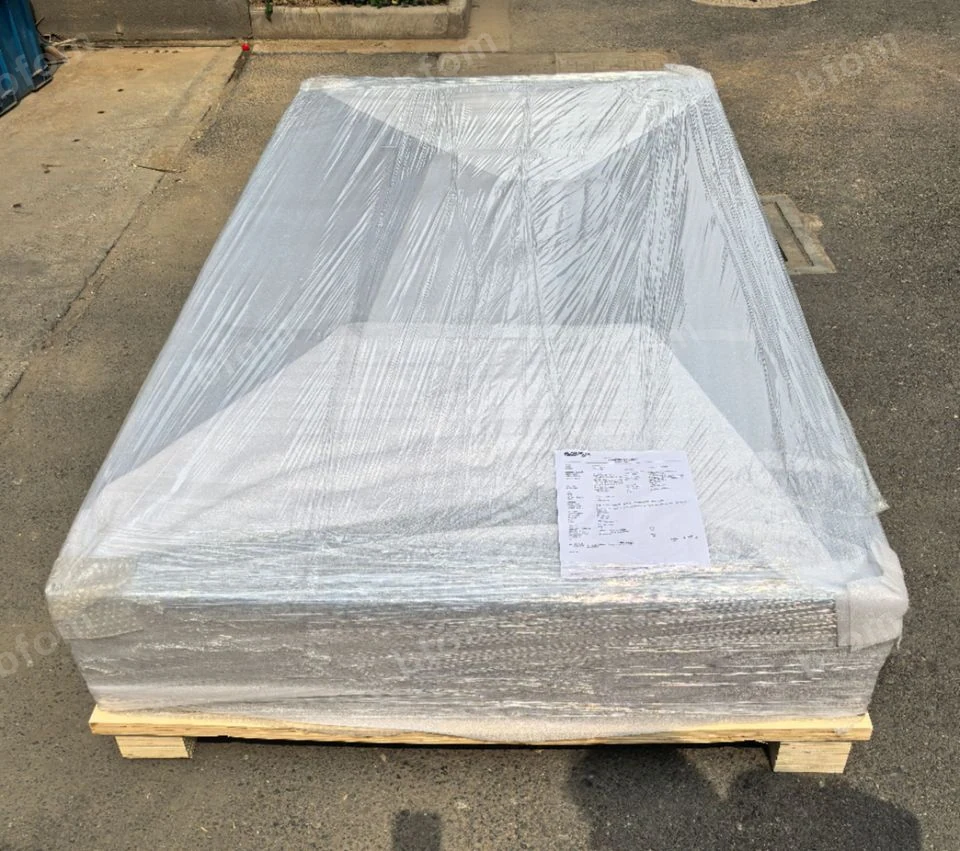
Representative production photographs. Project-specific records are not published because they can contain customer drawings and contact information.
For client inspection or pre-shipment acceptance, the record should allow the buyer and supplier to trace the same item. Recommended fields are purchase order, panel ID, approved sample reference, nominal and measured thickness, measured dimensions, face/edge result, lighting result where applicable, packing result and release date.
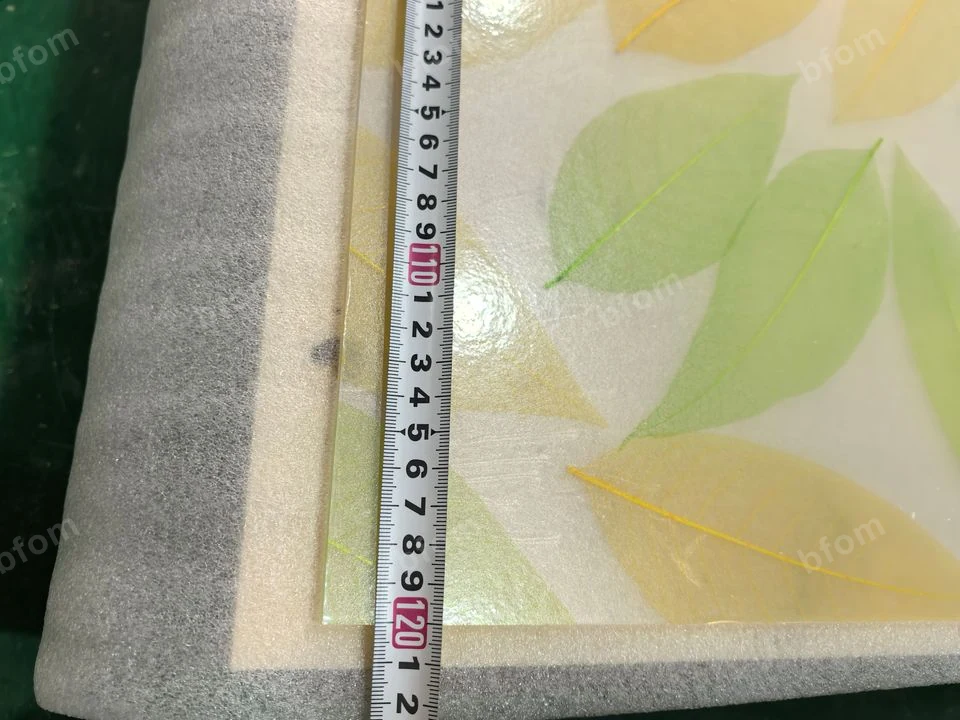
Instrument readings and units should be recorded. A photograph with a ruler is useful context but is not a substitute for a calibrated measurement and a signed acceptance criterion.
The available fire report (No. 2022100756) tests a client-delivered 4 mm PETG resin-panel specimen under GB 8624-2012. It records B-s2, d0, t1 and a B1 difficult-to-ignite classification for that tested construction. It does not establish the classification of every material or thickness in the range.
The available SGS inspection report (No. SHMR220020543401) tests a nominally 4 mm resin-panel sample for heat-deflection temperature, tensile and flexural properties and light transmittance. It does not establish FDA food-contact approval, LEED contribution or recycled content.
Send the required standard, destination, material, thickness and application. The relevant report or the need for additional testing will be confirmed in writing.
Send the standard, accepted tolerances, panel schedule, destination and required inspection method. The quotation can state the agreed inspection and document scope.
Contact the technical team